Description
Product Overview
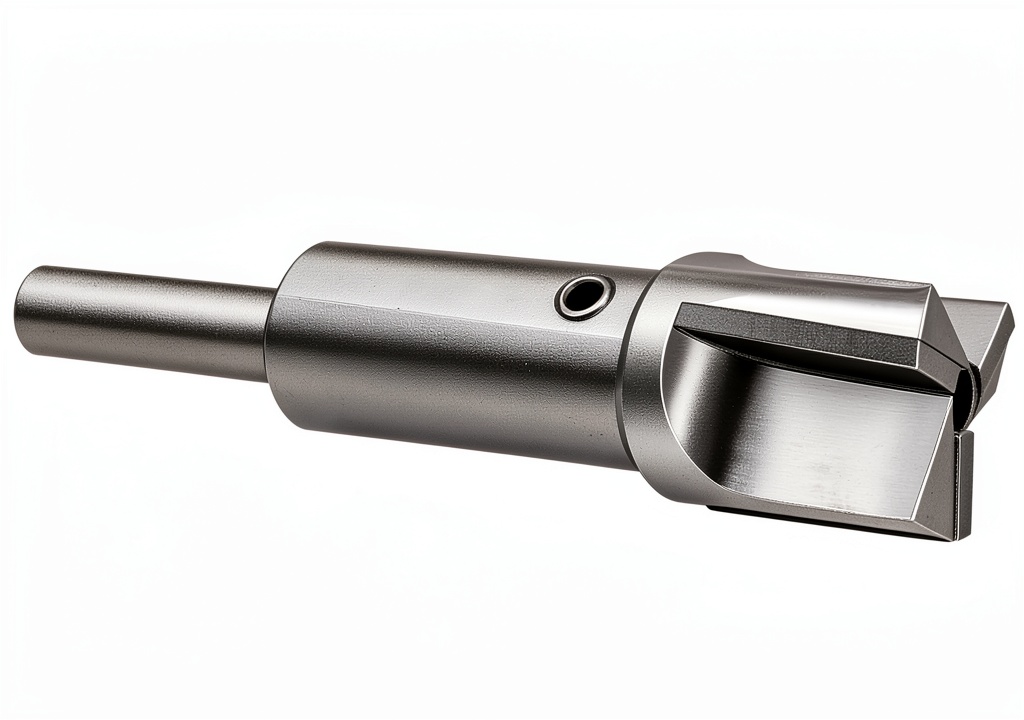
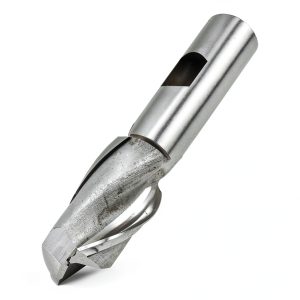
The Super Tool 3/4″ aircraft counterbore is engineered for high‑precision machining where space constraints demand a reduced shank size. Constructed from premium carbide, the cutting tip maintains sharpness even under demanding conditions, delivering consistent material removal and a superior surface finish. With a 1/4″ shank diameter, the tool easily fits into compact collet chucks, making it ideal for CNC machines, manual mills, and specialized aerospace equipment. The overall length of 2.75 inches and a .75″ cutting diameter provide a balanced reach that supports both deep counterboring and shallow spotfacing operations. Tolerances are tightly controlled: the tool diameter tolerance is +0.001″/‑0″ and the shank tolerance is +0″/‑0.001″, ensuring a predictable fit and repeatable results across multiple setups.
Usage
This counterbore excels in environments where precision and reliability are paramount. Aerospace manufacturers use it to create clean, accurately sized counterbores for fastener installation, ensuring structural integrity and compliance with strict industry standards. In industrial settings, the tool is employed for spotfacing on engine components, gear housings, and heavy‑duty brackets where a uniform bearing surface is required. The reduced shank design allows the tool to be used on machines with limited spindle clearance, such as compact CNC routers or older manual mills that cannot accommodate larger shank diameters. The pilot hole diameter of 3/16″ means the tool can start cutting from a pre‑drilled hole, reducing the risk of material deformation and extending tool life. Whether you are performing a single‑piece repair or a high‑volume production run, the counterbore delivers consistent performance.
Why Choose Us
Choosing the Super Tool aircraft counterbore means selecting a product backed by decades of machining expertise and rigorous quality control. Each tool is manufactured in the United States, adhering to ISO‑9001 standards, and undergoes a multi‑stage inspection process that includes dimensional verification, hardness testing, and functional performance checks. The carbide tip is heat‑treated to achieve a hardness of 1,200 VHN, providing exceptional wear resistance and reducing the frequency of tool changes. Additionally, the set screw mechanism allows users to secure a pilot or drill bit directly to the shank, offering flexibility for custom machining strategies and minimizing setup time. Our dedicated technical support team is available to assist with tool selection, setup advice, and troubleshooting, ensuring that you get the most out of your investment.
Key Features
- Carbide‑tipped cutting edge delivers long‑lasting sharpness and superior surface finish.
- Reduced 1/4″ shank enables use in machines with limited spindle clearance.
- Three‑flute geometry provides smooth chip evacuation and reduces vibration.
- .75″ cutting diameter and 3/16″ pilot hole support a wide range of counterboring applications.
- Set screw allows secure attachment of pilot or drill bits for added versatility.
- U.S. manufacturing ensures strict quality control and consistent performance.
- Comes with comprehensive technical support and after‑sales service.
FAQ
What material is the cutting tip made of?
The cutting tip is made of high‑grade carbide, heat‑treated to achieve a hardness of approximately 1,200 VHN, which provides excellent wear resistance and maintains sharpness during extended use.
Can I use this counterbore on a standard 1/2″ collet chuck?
Yes. The 1/4″ shank diameter fits comfortably within a 1/2″ collet chuck, allowing you to secure the tool without additional adapters while still benefiting from the reduced shank design.
Is a pilot hole required for operation?
A pilot hole of at least 3/16″ is recommended to start the cutting process cleanly. The tool includes a set screw that can hold a pilot or drill bit in place, ensuring accurate alignment and reducing the risk of material deformation.
What is the recommended cutting speed for aluminum?
For aluminum alloys, a cutting speed of 150–200 SFM (surface feet per minute) is typically effective. Adjust feed rates based on material thickness and machine rigidity to achieve optimal chip formation.
How do I maintain the tool for long‑term use?
After each use, clean the cutting tip with a solvent to remove chips and coolant residue. Inspect the carbide tip for wear and replace the tool if the cutting edge becomes dull or damaged. Store the tool in a dry environment to prevent corrosion of the shank.
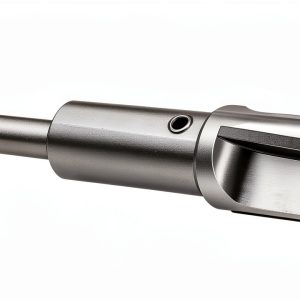
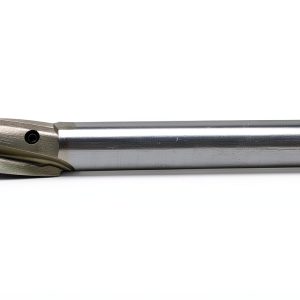 Vermont Gage 3/8" Interchangeable Pilot Counterbore
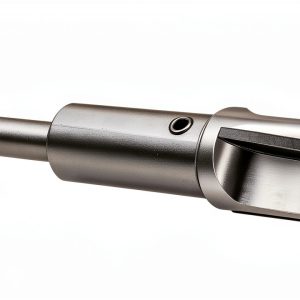 Aircraft Counterbore 13/32" Carbide Tipped Shank 1/4" Super Tool
Reviews
There are no reviews yet.